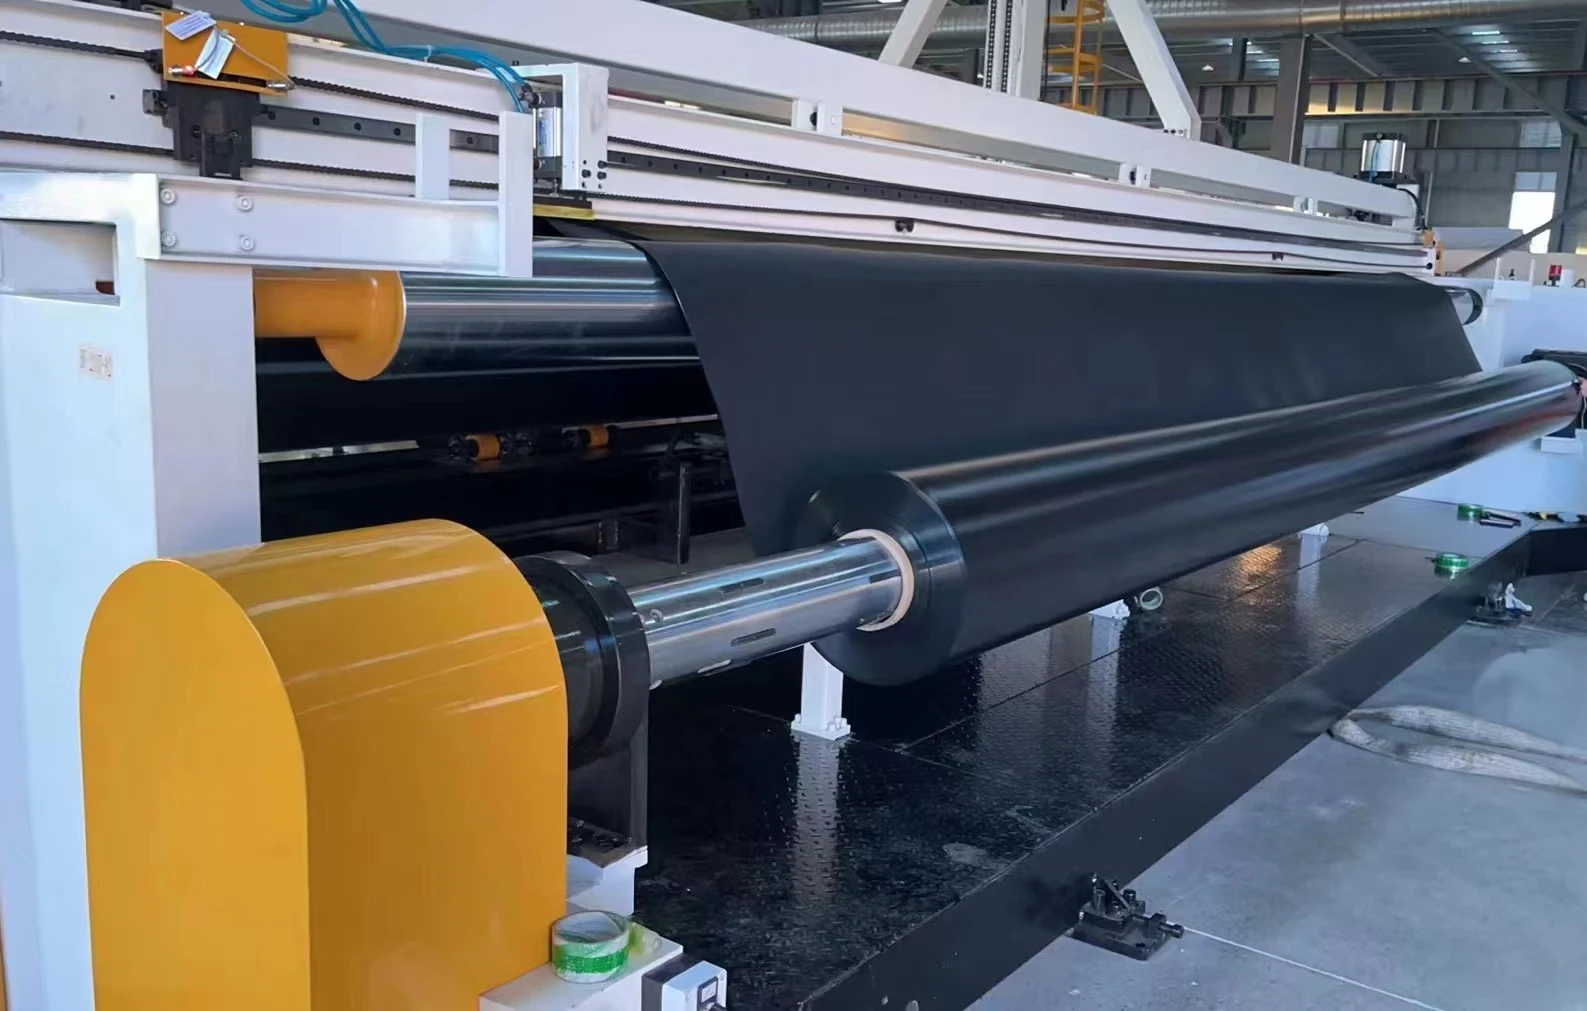
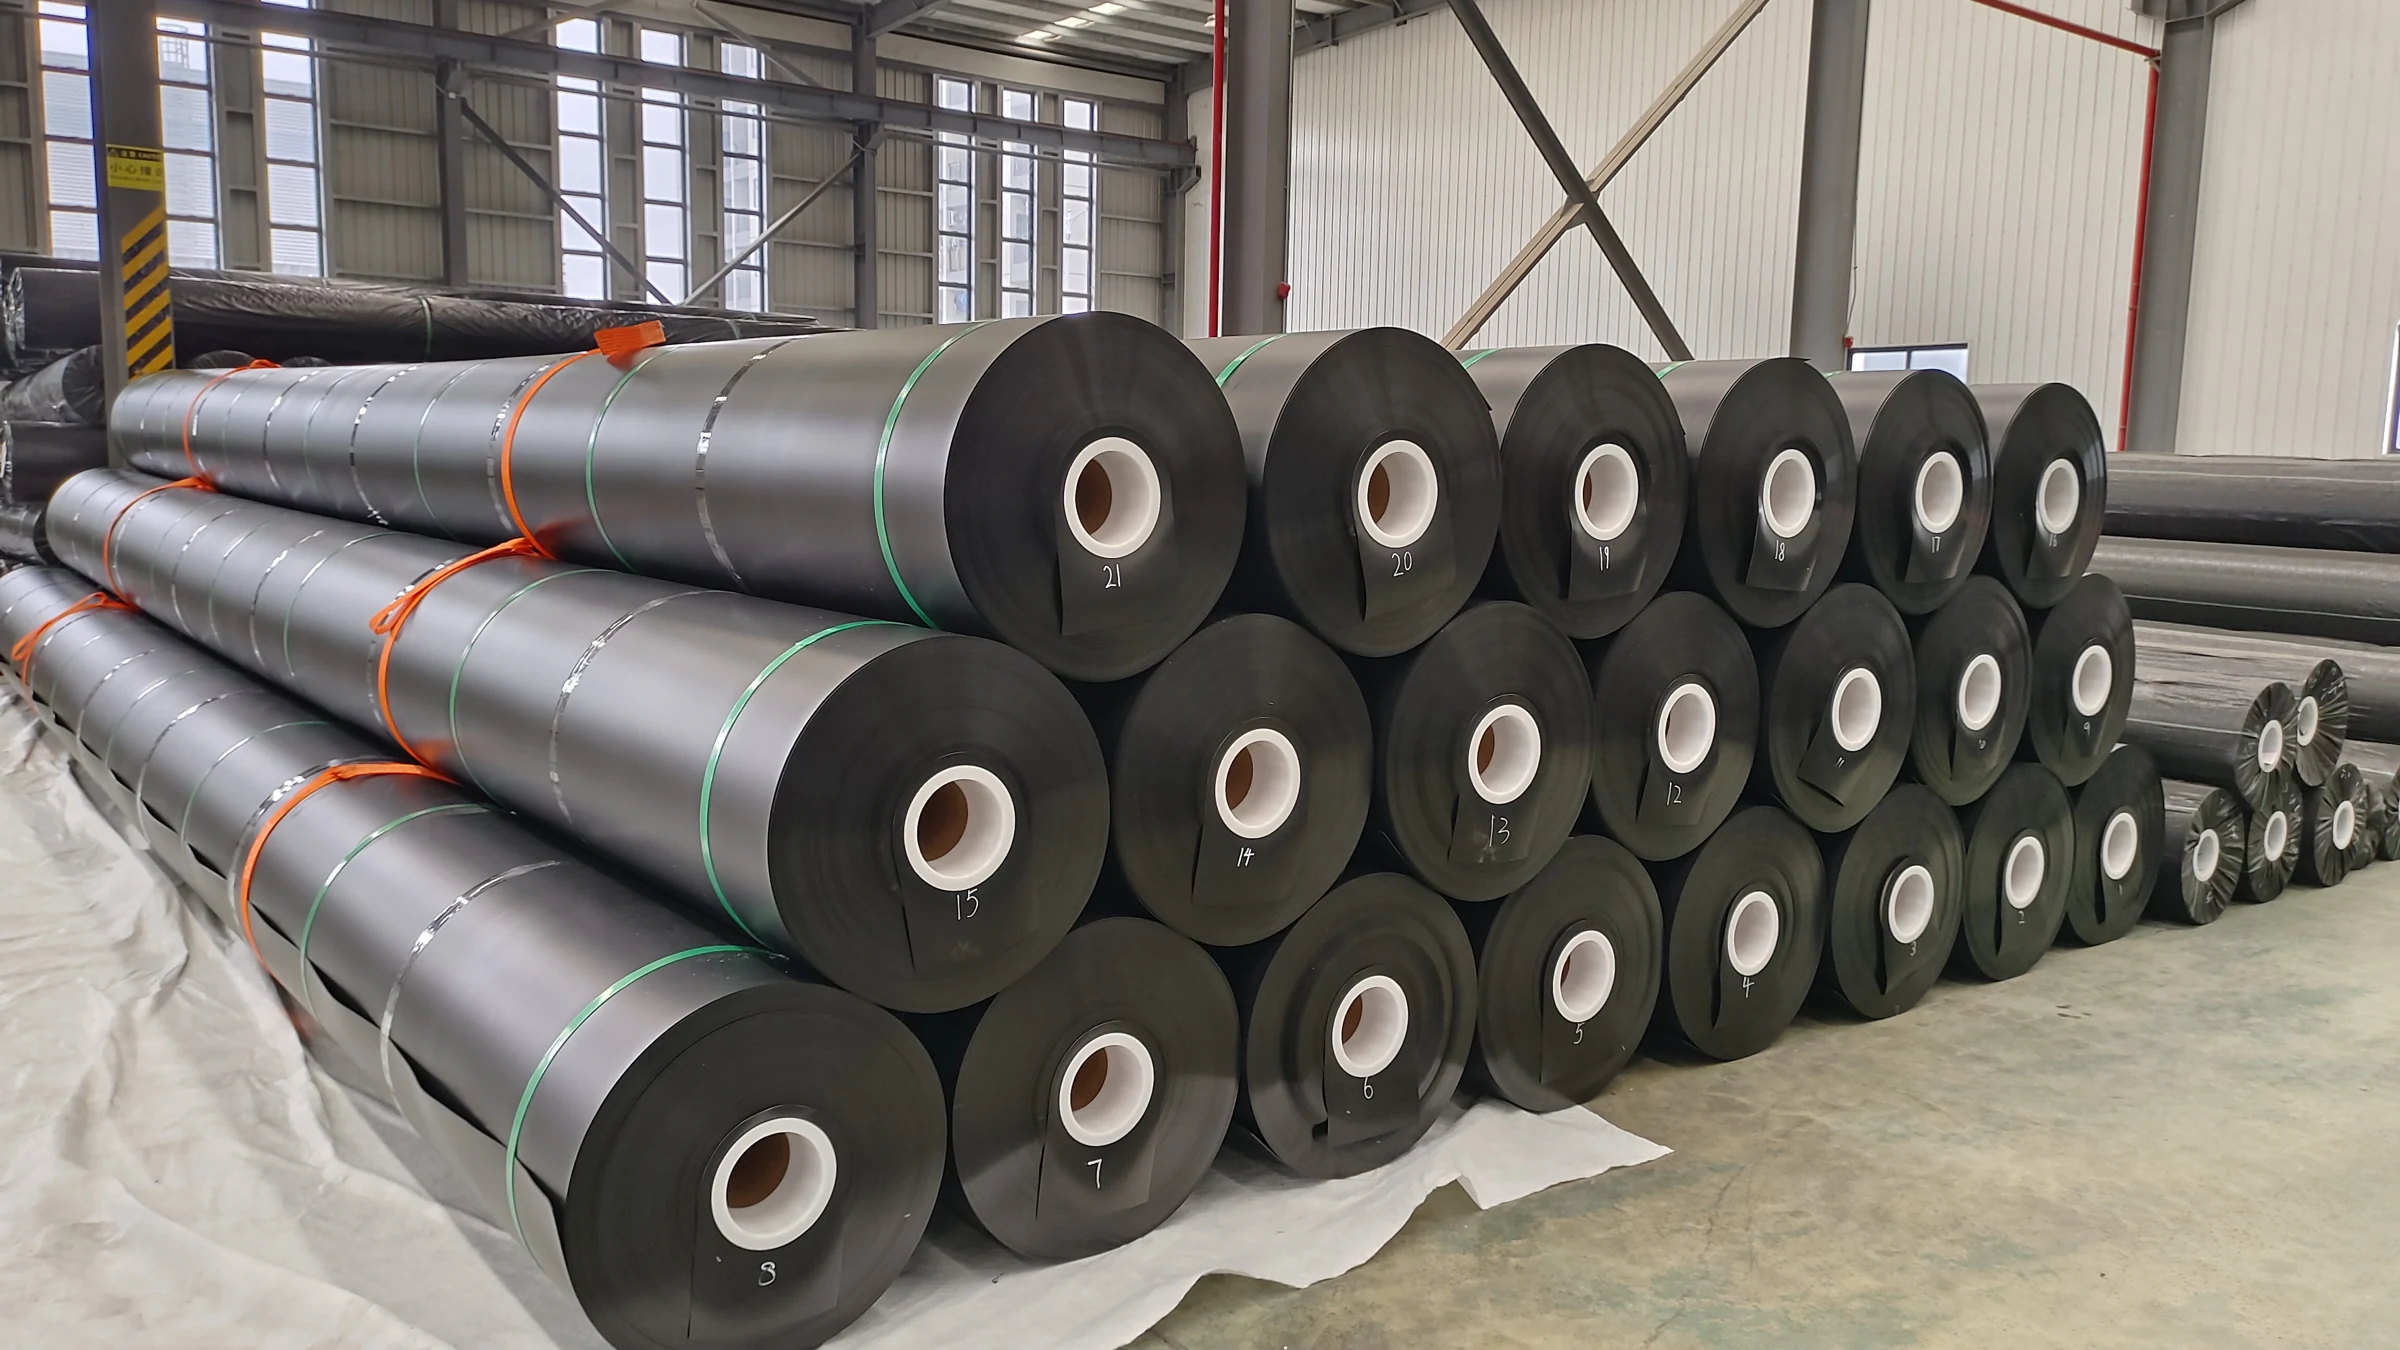
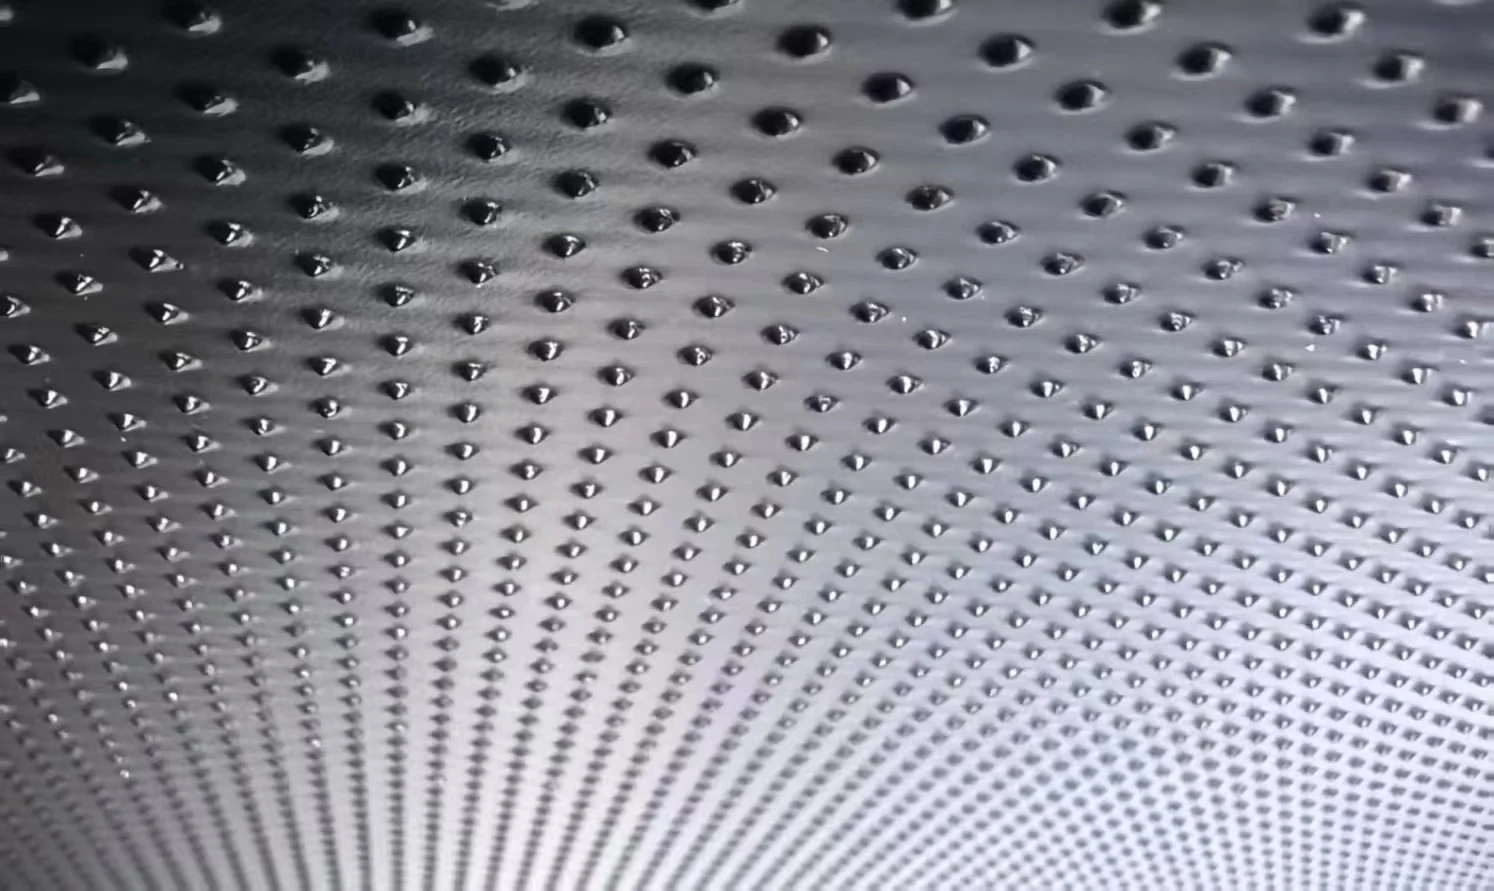
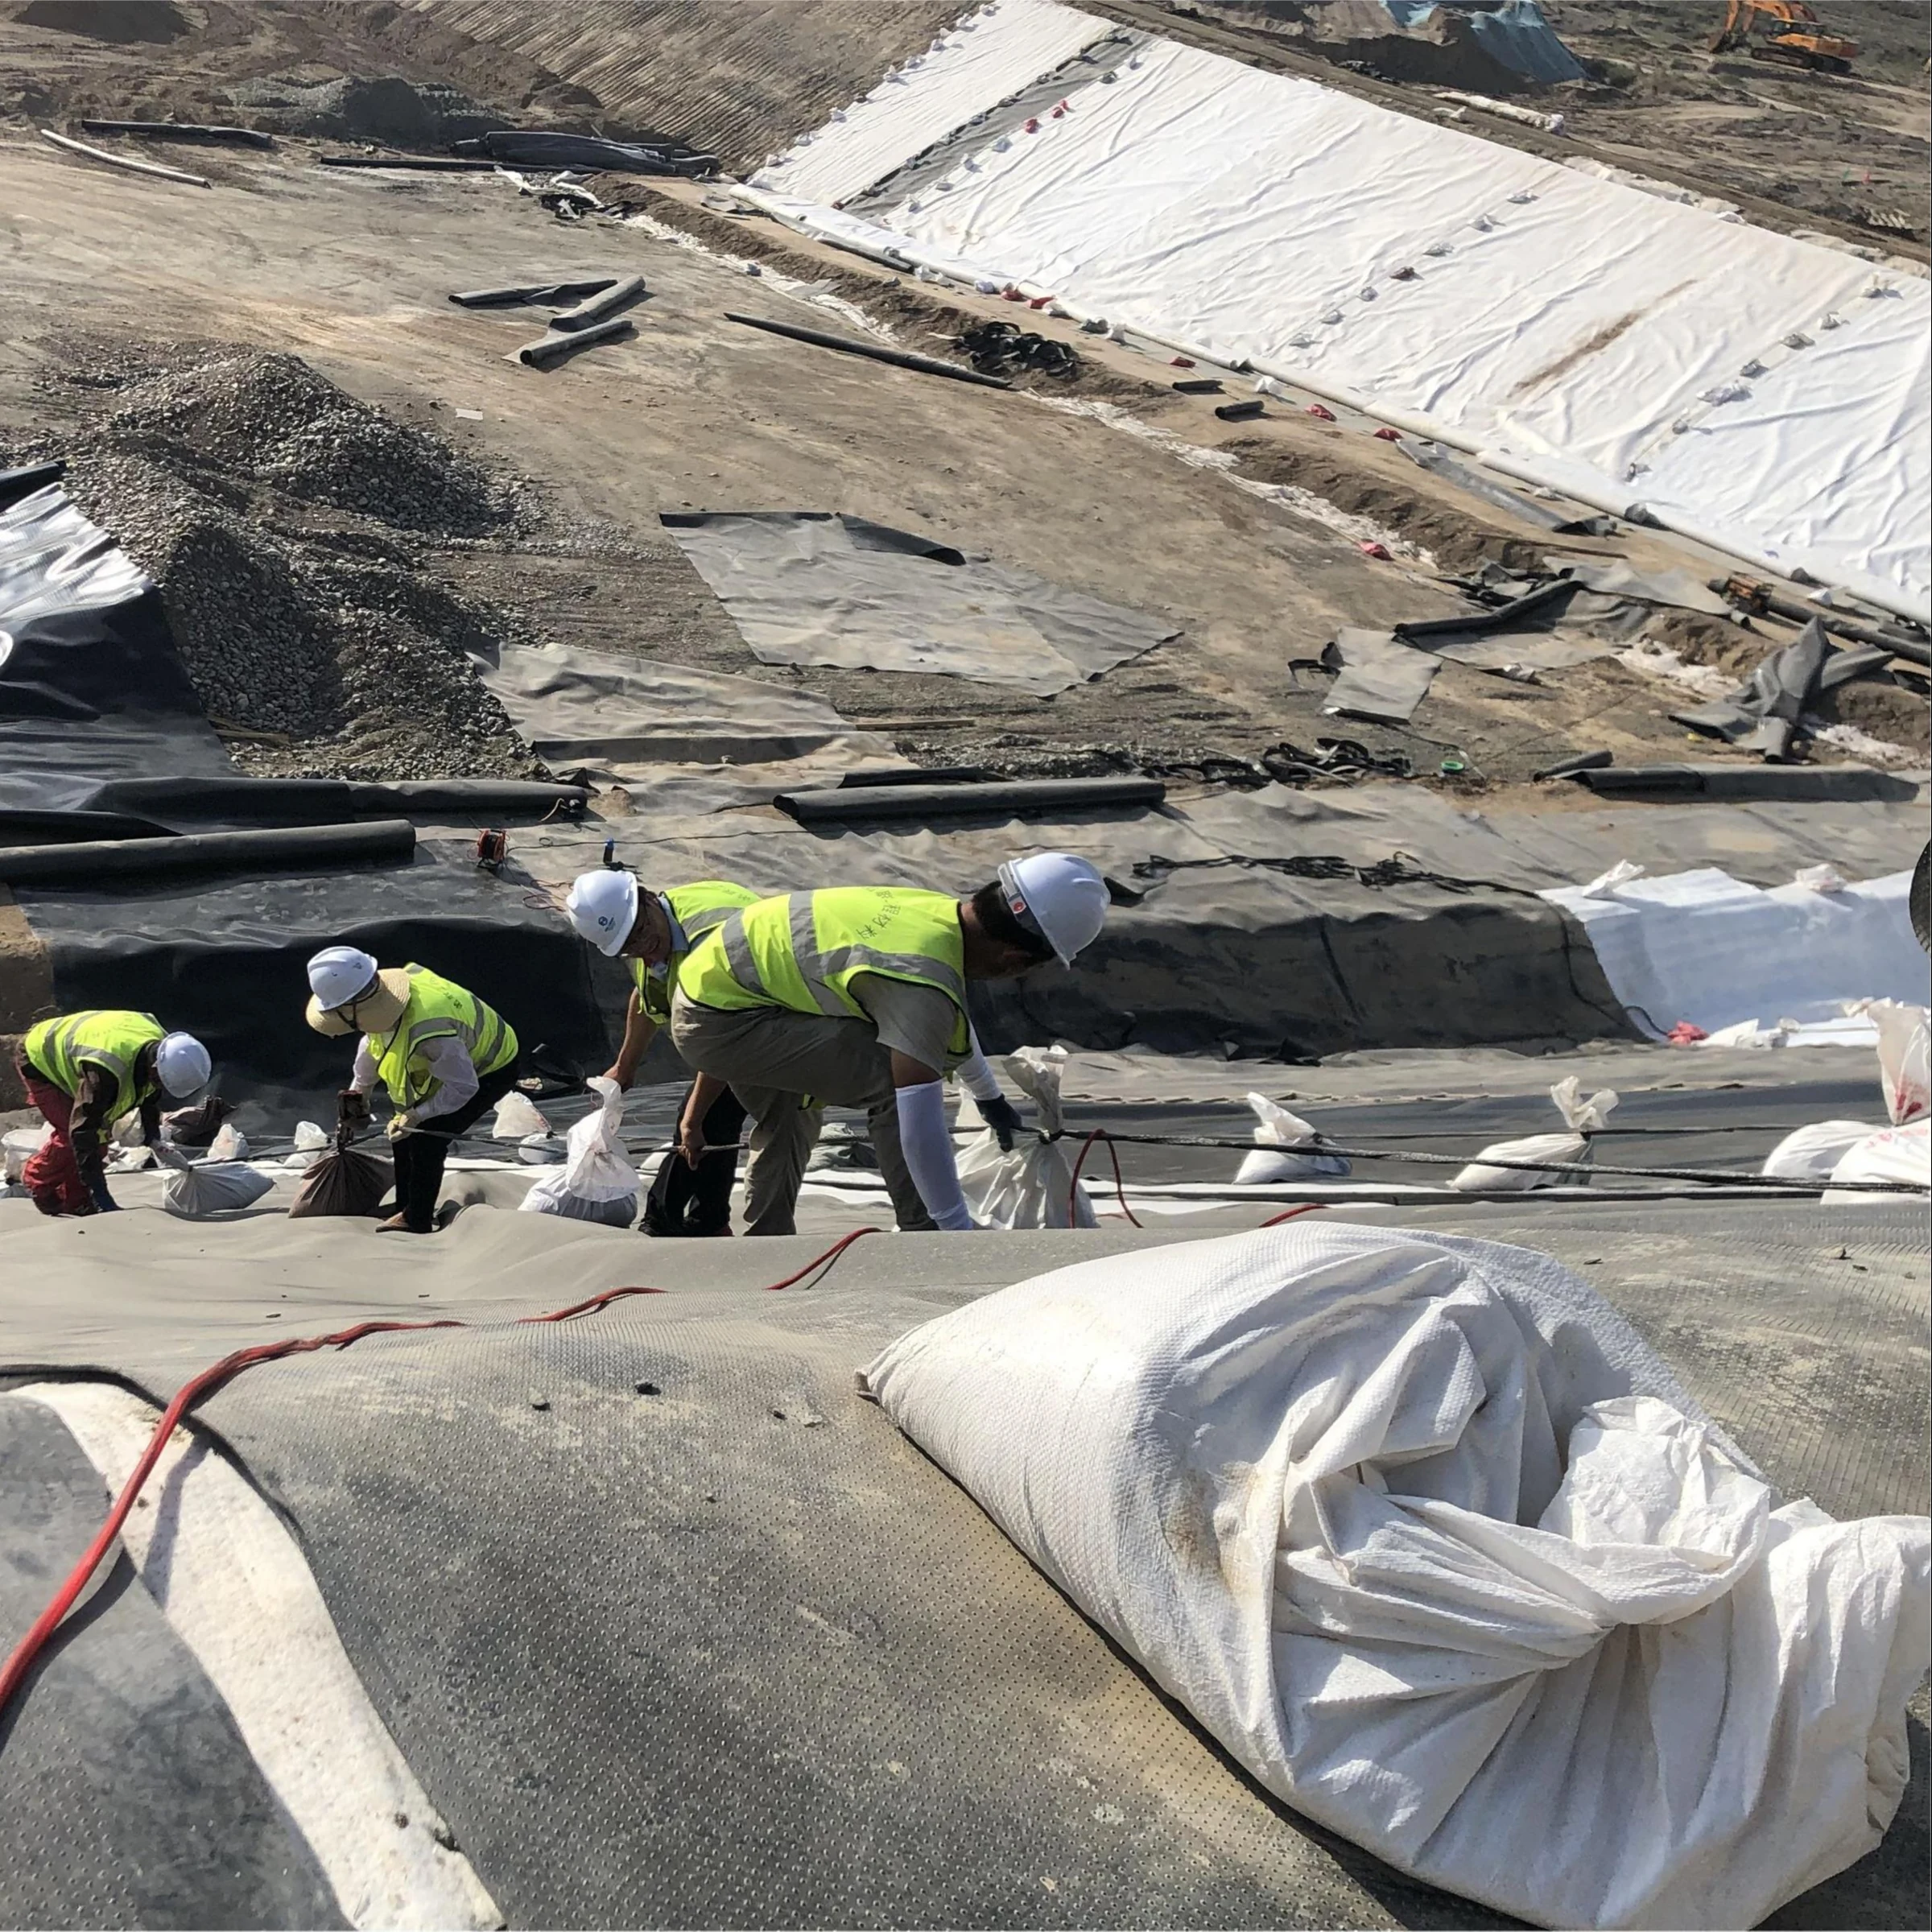

Vet an HDPE geomembrane manufacturer by verifying the proposed product, traceable quality records and deliverable production capacity against your project’s requirements. A resin brand, large machine, certificate or advertised square-meter output is not enough. Resolve material approval, delivery milestones, inspection rights and nonconforming-product procedures before committing the order.
This guide addresses supplier qualification for large orders. For inspection of an individual delivery, use the HDPE roll-quality checklist; for offered dimensions and grades, review the HDPE product page.

Start with a common technical requirement
Give every bidder the same drawings, exposure conditions, surface finish, thickness, quantities, roll-handling limits and adopted specification edition. Ask suppliers to identify deviations explicitly. A lower quotation for a different thickness, missing testing or a different delivery basis is not an equivalent offer.
| Qualification area | Evidence to request | Decision supported |
|---|---|---|
| Product identity | Offered grade, formulation identifier, surface, thickness and data sheet | The proposal matches the design rather than a generic brochure. |
| Manufacturing control | Relevant production records, test plan, calibration and nonconformance examples | The plant can repeatedly make and release conforming material. |
| Traceability | Example linking resin lot, production lot, roll label and report | A questionable batch can be identified and isolated. |
| Capacity | Recent run records for comparable grades, available slots and commitments | The promised quantity can be released by the required dates. |
| Delivery | Packaging, loading limits, shipping plan, document list and contingency | Production output can actually reach the site in usable condition. |
Check resin and formulation control without relying on brand names
Ask how incoming resin is identified, stored, released and linked to finished rolls. Review supplier certificates of analysis and the manufacturer’s incoming checks. A named petrochemical supplier is useful traceability information, but does not independently prove the finished sheet meets the project specification.
GRI-GM13 Revision 19 distinguishes base resin from formulated HDPE sheet. It permits limited, suitable production rework with virgin resin and prohibits post-consumer resin. Therefore a contract requiring no rework is a separate, stricter purchasing requirement. State it explicitly rather than treating “GM13 compliant” and “no rework” as identical.
Request the melt-flow test condition with every result. Values measured at different temperatures or loads cannot be compared as if they were the same property. Do not infer contamination from density alone, or infer guaranteed stress-crack performance from comonomer names. Investigate unexplained changes using formulation records and relevant finished-sheet tests.
Agree when changes in resin grade, additives, production location or formulation require notification and renewed approval. Protect proprietary formulations through the agreed disclosure process while still obtaining the evidence necessary for material acceptance.
Distinguish certificates from product test evidence
A quality-management certificate concerns the management system and its stated scope. It is not a report for the delivered rolls. Check issuer, validity, legal entity, manufacturing location and scope rather than counting logos.
The GAI laboratory accreditation program recognizes capability for individual test methods; it does not certify each reported result. If a supplier claims laboratory accreditation, verify the laboratory and the relevant test scope. Do not imply Jinseed or every supplier must hold a particular accreditation unless the project requires it and the claim is documented.
Specify which properties need manufacturing QC, independent conformance testing or project-specific performance assessment. Standard OIT and HP-OIT are different tests, and the adopted specification controls the applicable option. A high OIT value or a 500-hour stress-crack result does not independently establish a 50-, 100- or 200-year field life. ASTM D8117 explains the limitations of life predictions from OIT.
Calculate deliverable capacity from the offered thickness
Ask for net, accepted output for the actual grade and thickness—not simply extrusion capacity or the sum of all machine nameplates. Account for downtime, changeovers, trim, rejected material, quality-release delays and existing orders. Do not deduct a loss twice if it is already included in the reported net output.
Illustrative calculation: assume 2,000 kg/h gross output, 24 scheduled hours/day, a combined net-output factor of 0.85, 1.5 mm sheet and 940 kg/m³ sheet density. The sheet mass is 940 × 0.0015 = 1.41 kg/m². Accepted area is 2,000 × 24 × 0.85 ÷ 1.41 ≈ 28,936 m²/day. One million square meters would require about 34.6 production days if that capacity were dedicated to the order. This excludes approval and shipping time and is not a Jinseed capacity claim.
An independent line-speed check uses net width × speed × operating minutes. At an assumed 7.5 m net width and 6 m/min, one uninterrupted hour produces 2,700 m², before rejection or other losses. Reconcile mass-based and area-based records using consistent thickness, density and operating time.
Check inventory and shipping constraints
Usable resin inventory divided by daily consumption gives a stock-coverage estimate. Three fully usable 200-tonne silos serving 120 tonnes/day provide 5 days, not a delivery guarantee. Deduct unavailable or incompatible inventory and compare coverage with confirmed replenishment lead times. Rail access, bagged resin or bulk delivery alone does not determine product quality.
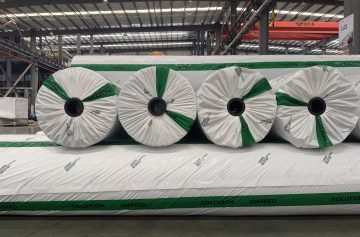
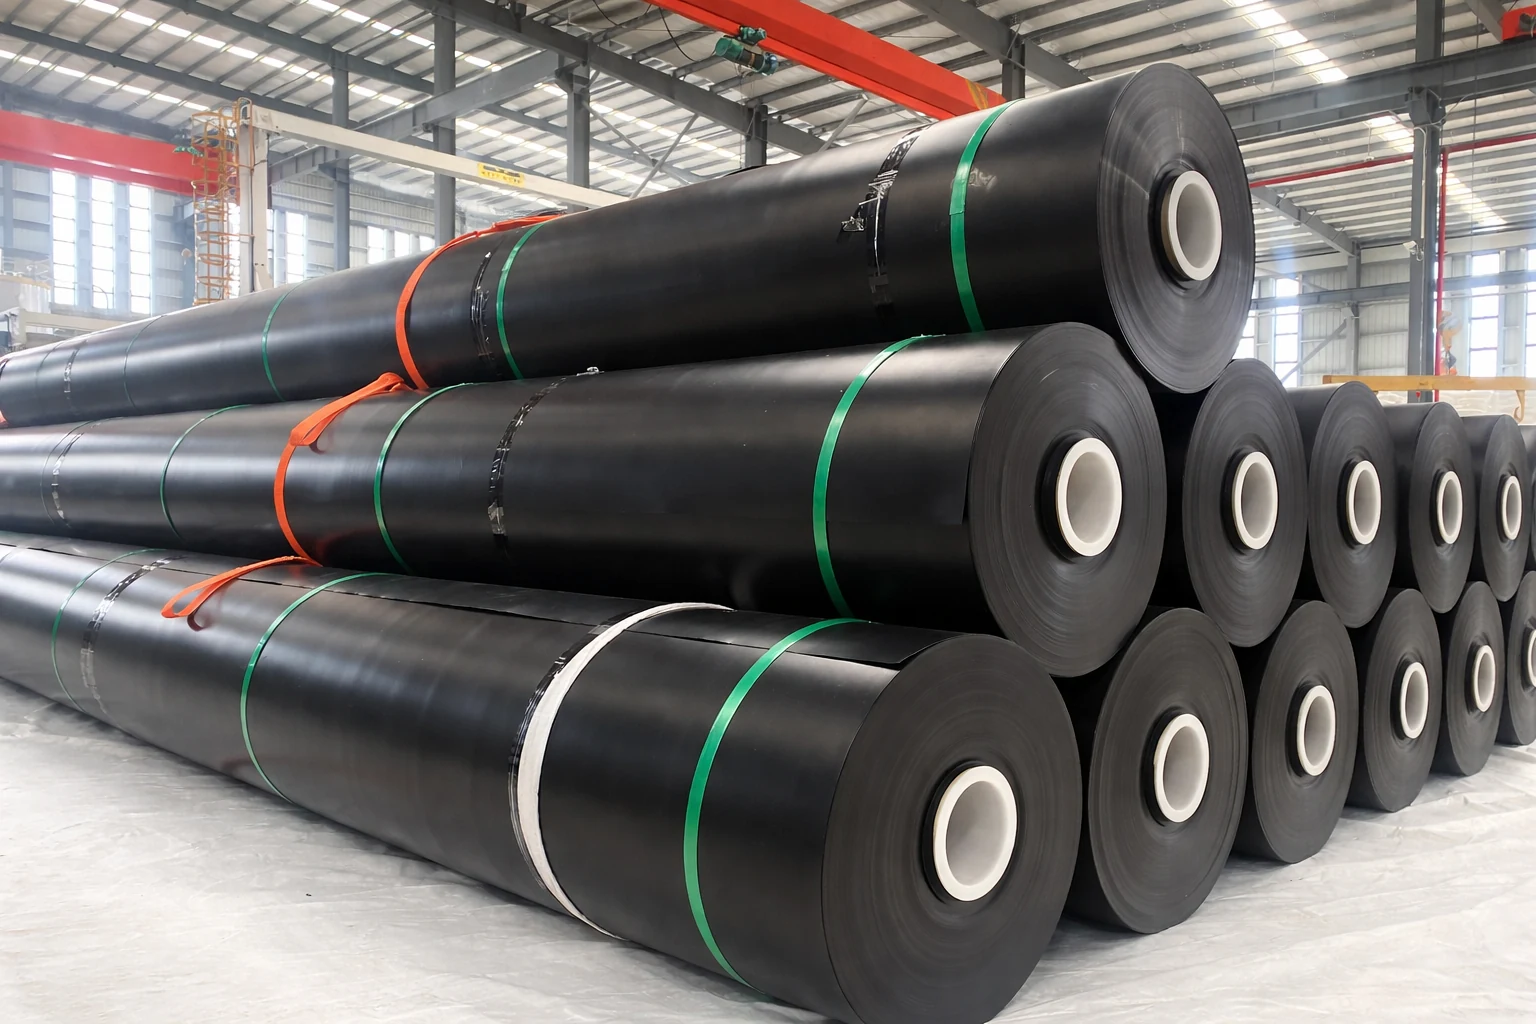
Agree roll mass, dimensions, cores, lifting arrangements and container loading with the site and carrier. Container counts depend on payload, roll geometry and the approved loading arrangement. Do not apply an unsupported universal number of containers per day.
Make the QC plan and release process auditable
Require a matrix connecting each property to its test method, applicable acceptance value, sampling basis, frequency, responsible party and record. Keep smooth and textured requirements separate. The current GM13 tables and project specification govern; a copied table of “typical factory frequencies” should not replace them.
- Approve the material submittal and sampling plan before production.
- Trace each delivery roll to the production lot and the tests that actually represent it.
- Identify hold points and who can release material after a failed or missing result.
- Agree sample retention, storage, retesting and record-retention requirements.
- Keep replacement rolls and repairs traceable through final acceptance.
Not every test is performed on every roll. A report should accurately identify the tested population and represented rolls rather than imply complete roll-by-roll testing when only batch samples were tested.
Compare commercial commitments after technical qualification
Request a dated production and shipping schedule, progress reporting, packaging responsibilities, delivery basis and documented exclusions. For reserved stock, define identification, release and storage arrangements. Review the actual warranty terms, covered defects and remedy; do not equate a warranty period with proven service life or assume a universal industry warranty.
Send Jinseed the project specification and required delivery sequence to request an offer with supporting documents. Keep unverified requirements open in the review record until the authorized project reviewer accepts the evidence.