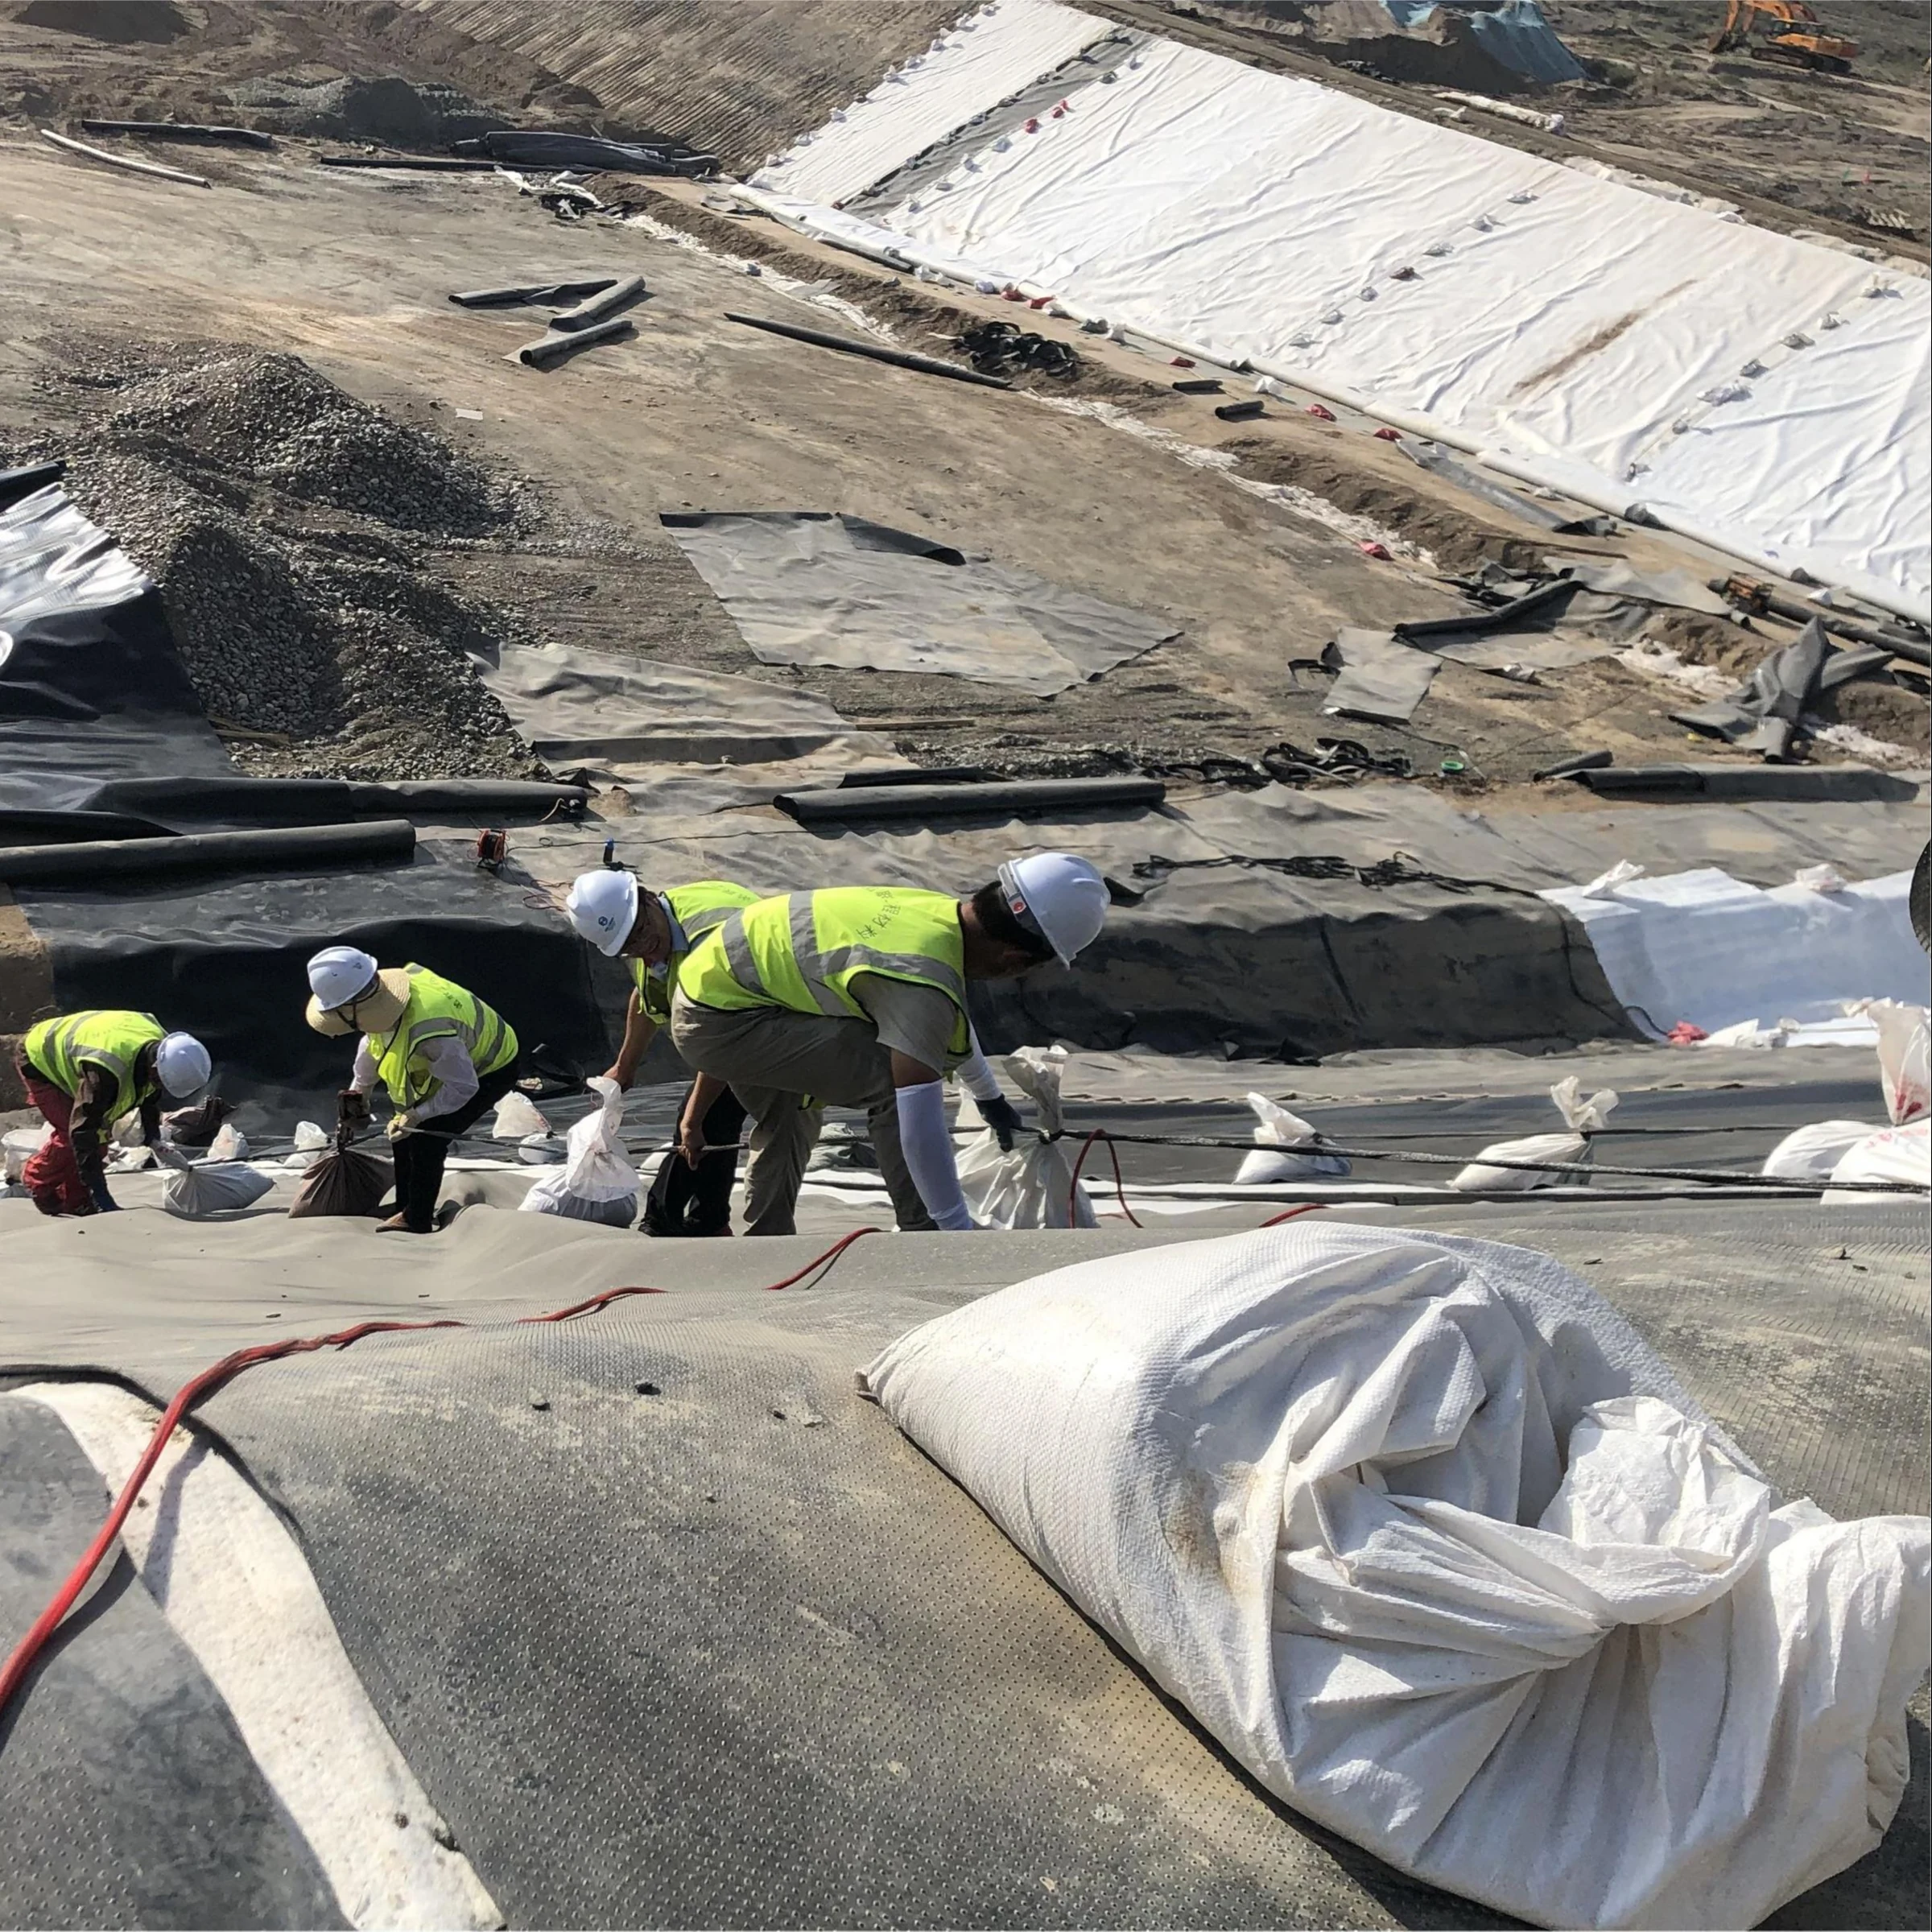

Heap leach pad liner testing combines three different checks: seam continuity, seam strength and the integrity of the installed sheet. An air-channel or vacuum test can identify certain seam discontinuities; destructive peel and shear testing assesses sampled welds; an appropriate electrical leak location survey can find breaches in the installed barrier. None of these alone proves that an entire heap leach facility is ready for operation.
This guide is for construction quality assurance (CQA) reviewers, installation contractors and mine procurement teams. Agree the test methods, acceptance criteria, sampling plan and release authority before welding begins. Material selection is covered separately in our heap leach geomembrane selection guide.
Seam Testing
What each inspection can establish
| Check | Purpose | Important limitation |
|---|---|---|
| Visual inspection | Find contamination, damaged sheet, wrinkles, incomplete welds and unsuitable details. | A tidy-looking weld may still have a strength or continuity defect. |
| Dual-track air-channel test | Assess continuity of an accessible channel between parallel weld tracks. | Does not measure weld strength; an obstructed channel can leave part of the seam untested. |
| Vacuum chamber test | Assess accessible seams, patches and suitable details for bubble indications. | The chamber must seal against the surface; corners, curved details and highly extensible sheet can limit use. |
| Destructive peel and shear tests | Assess sampled weld strength and failure behavior. | A sample represents its location and the agreed sampling plan, not every metre of seam. |
| Electrical leak location (ELL) | Locate breaches in an installed electrically insulating barrier under suitable site conditions. | Sensitivity depends on the method, electrical contact, cover, isolation and demonstrated survey conditions. |
Non-destructive testing: dual-track seams
ASTM D5820-95(2023) addresses pressurized air-channel evaluation. It assesses continuity and watertightness of the tested seam channel, not physical seam strength, and is not a replacement for destructive testing.
- Identify the seam and its limits on the panel plan. Confirm that the channel is accessible and that the selected test arrangement covers the complete intended length.
- Use the pressure, stabilization period, observation duration and allowable pressure change specified in the approved procedure for that material and equipment.
- Record initial and final readings, elapsed time, temperature conditions, gauge identification and the operator. Investigate equipment leakage, end seals and blocked channels before deciding whether the weld passes.
- Demonstrate channel continuity in accordance with the procedure, identify any untested segment, and test it separately.
- Mark failures, record repairs and repeat the applicable test before releasing the seam.
A value such as 30 psi or 0.25 MPa is not a universal setting for every thickness and temperature. For unit checking, 30 psi is approximately 207 kPa, while 0.25 MPa is 250 kPa, approximately 36.3 psi. These are conversions, not recommended test pressures. Temperature changes can affect a closed air-channel reading; do not automatically subtract a guessed temperature allowance to turn a failing test into a pass.
Vacuum testing and complex details
ASTM D5641/D5641M-25 covers vacuum-chamber evaluation of suitable seams, patches and defects. Prepare the surface, apply the approved wetting solution, establish the specified vacuum and inspect for continuing bubble formation. Use overlapping test positions so that the required area is covered. Vacuum level and observation time must come from the governing procedure, not a generic internet checklist.
If a chamber cannot seal around a penetration or corner, the CQA plan needs a suitable alternative detail and test method. Do not treat conductive-backed sheet testing as interchangeable with spark testing of a specially prepared seam. ASTM D6747-25 helps select electrical leak location techniques for the actual lining configuration. Electrical testing should be performed by qualified personnel using the approved equipment and safety procedure.
Destructive Testing
Sampling standards and traceability
Establish sample selection, frequency, dimensions, conditioning and laboratory responsibilities in the CQA plan. Include both production sampling and additional investigation when welding conditions or results indicate a problem. A statement that “one sample every 500 ft is required everywhere” is too broad: 500 ft equals 152.4 m, not exactly 150 m, and the contractual sampling rule controls.
GRI-GM19a, Revision 10 (18 March 2021) specifies seam properties for thermally bonded homogeneous polyolefin geomembranes. It explicitly does not establish a field destructive-sampling interval. Its tables also distinguish material, thickness and seam method. Confirm the edition incorporated into the project specification rather than transferring one table entry to all welds.
Label samples with project, panel and seam IDs, location, date, material, thickness, welder and machine. Record sample custody and which portions go to the installer, CQA reviewer and laboratory. Repair every extraction location and record its retest; sampling must not leave an undocumented opening.
Peel, shear and failure behavior
ASTM D6392-25 describes destructive tests for nonreinforced geomembrane seams produced by thermo-fusion. The report should identify the method and include the required peel and shear results, separation and failure observations. Compare them with the specified acceptance criteria for the exact material and seam type.
Keep force and force per specimen width separate. For an illustrative specimen 25 mm wide carrying 500 N, the normalized result is 500 ÷ 25 = 20 N/mm, or 20 kN/m. This calculation does not establish a pass threshold. Do not substitute an average result for an individual-specimen rule, or use a shear result as if it were a peel result. For dual-track seams, evaluate the tracks as required by the applicable method.
Handling a non-conforming seam
Identify and hold the affected area. The responsible CQA reviewer should determine the extent of investigation and repair from the failed result, neighboring results, seam records and governing plan. Do not assume that a fixed short patch or a second passing sample automatically closes the original failure.
Repair preparation, compatible patch material, geometry and welding settings must follow the approved procedure. Thermoplastic polyethylene welding relies on fusion; it is not a claim of chemical crosslinking. Avoid arbitrary grinding depths or temperatures that could reduce the parent sheet thickness or damage the material.
Post-Installation Phase
Leak location before and after protection placement
Plan the survey sequence before construction. Damage can occur while placing protection or drainage material after the initial weld tests. Where specified, survey after the relevant covering operation and before the next stage makes repairs impractical. Coordinate this hold point with the installer, earthworks contractor and CQA team.
ASTM D7007-24 addresses electrical methods for geomembranes covered with water or earthen materials. Method selection must suit the real layer arrangement. Dry nonconductive layers, poor electrical contact or unintended current paths can reduce detection capability. A claimed ability to find every 0.5 mm hole is not a defensible blanket guarantee.
Require a survey report showing the area actually tested, the site conditions, method, equipment, demonstrated sensitivity, exclusions, mapped indications and repair verification. ASTM D7909-21a(2025) discusses intentional leaks used to evaluate survey effectiveness. Any such verification must be agreed by the parties, documented and repaired; personnel should not cut arbitrary calibration holes into an accepted liner.
Final release checklist
- Accepted subgrade and material delivery records are traceable to the installed panels.
- Trial weld, production weld, continuity and destructive-test records cover the specified scope.
- Failures and exclusions have a documented disposition; repair locations and successful retests appear on the as-built plan.
- Penetrations, terminations, anchors and drainage interfaces match approved details.
- Protection placement and any required ELL surveys are accepted before further loading.
- The authorized reviewer has signed the release required by the contract and local permit. An ASTM test does not itself issue an operating permit.
After handover, follow a separate heap leach liner maintenance and monitoring plan. For general welding methods, see our geomembrane welding and seam testing guide.
Prepare the testing scope before ordering
Send the material specification, thickness, surface finish, panel layout and required CQA documents when requesting HDPE geomembrane. Agree which documents concern manufacturing quality and which tests must be performed on site. Contact Jinseed with the project requirements to confirm the proposed supply and documentation scope.